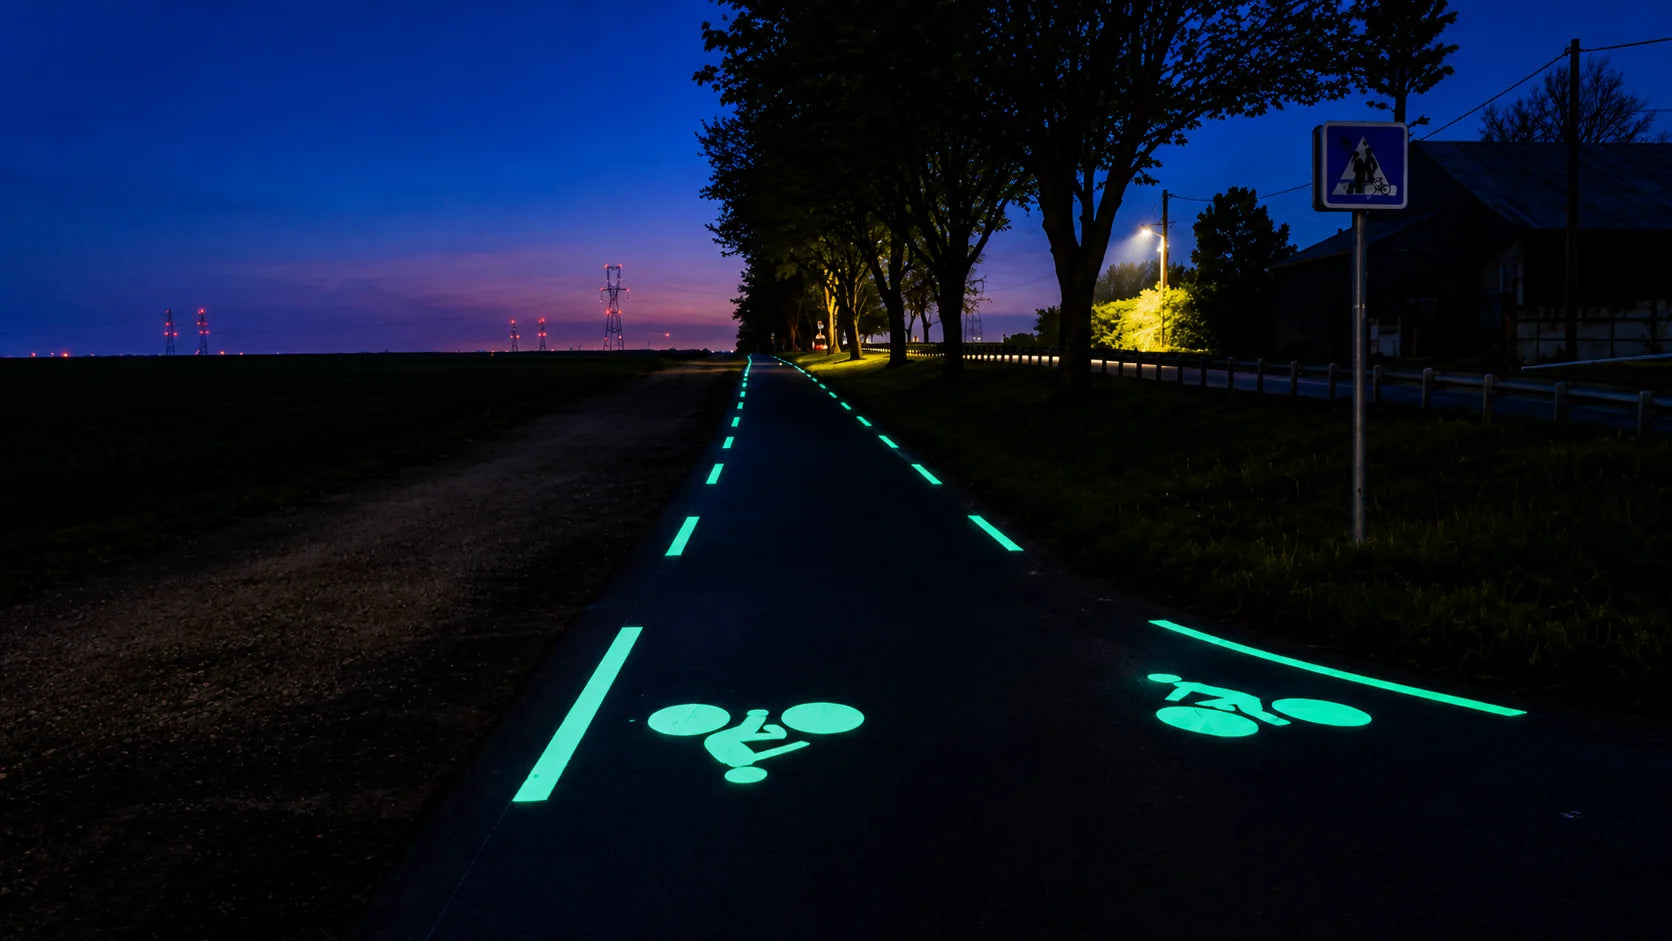
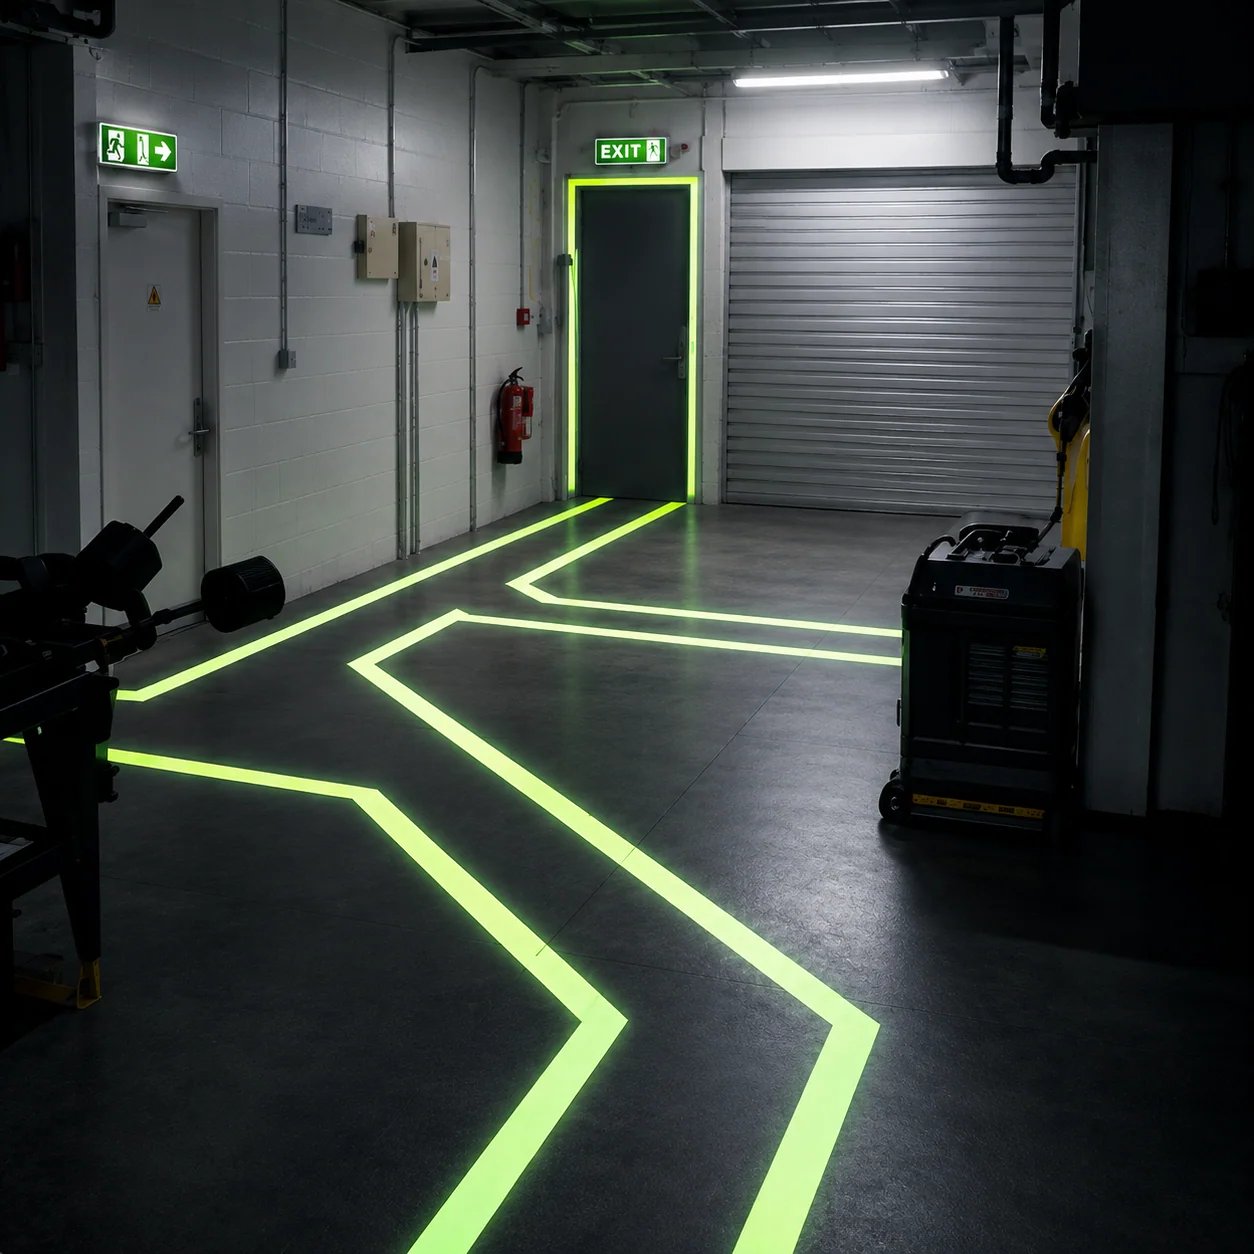
Photoluminescent marking for industrial floors can add low-level guidance in factories, warehouses, logistics centers, workshops and production facilities where pedestrians, forklifts, machines, storage areas, loading zones and emergency routes share space.
Conventional markings are usually easy to see under normal lighting, but may be harder to recognize during reduced lighting, a power interruption or in darker parts of a facility. Photoluminescent markings absorb daylight or suitable artificial light and release visible afterglow in darker conditions to help identify selected routes, boundaries, stairs, exits and safety zones. The afterglow itself needs no electrical power.
How photoluminescent industrial floor markings work
Photoluminescent floor marking is a coating or marking system containing light-storing luminous material. The basic process is:
Light Exposure → Energy Storage → Afterglow → Recharge
During normal factory or warehouse operation, ceiling lights can charge the material.
When the surrounding light level decreases, the stored energy is gradually released as visible glow. This is different from reflective marking, which depends on an external light source at the moment it is viewed.
Plan routes and boundaries around the facility
Industrial environments contain many visual zones that need to remain easy to understand. These may include:
- Pedestrian walkways
- Forklift lanes
- Emergency routes
- Machine boundaries
- Loading areas
- Storage zones
- Stair edges
- Exit paths
- Restricted areas
Photoluminescent markings can reinforce these areas when lighting conditions change.
Pedestrian Walkways
Pedestrian routes are one of the most practical applications. Luminous lines can be used along both sides of a walkway to create a continuous floor-level path. They may connect:
- Factory entrances
- Workstations
- Offices
- Storage areas
- Stairways
- Emergency exits
A continuous line is often easier to follow than isolated symbols.
Forklift and Vehicle Zones
Many industrial facilities use forklifts, carts, and internal vehicles. Photoluminescent markings can help define boundaries between:
Pedestrian Area | Vehicle Route | Restricted Zone
However, forklift traffic creates significant abrasion.
Markings placed directly under repeated wheel paths may wear faster. For this reason, the coating system should be selected according to the actual traffic level.
Emergency Exit Routes
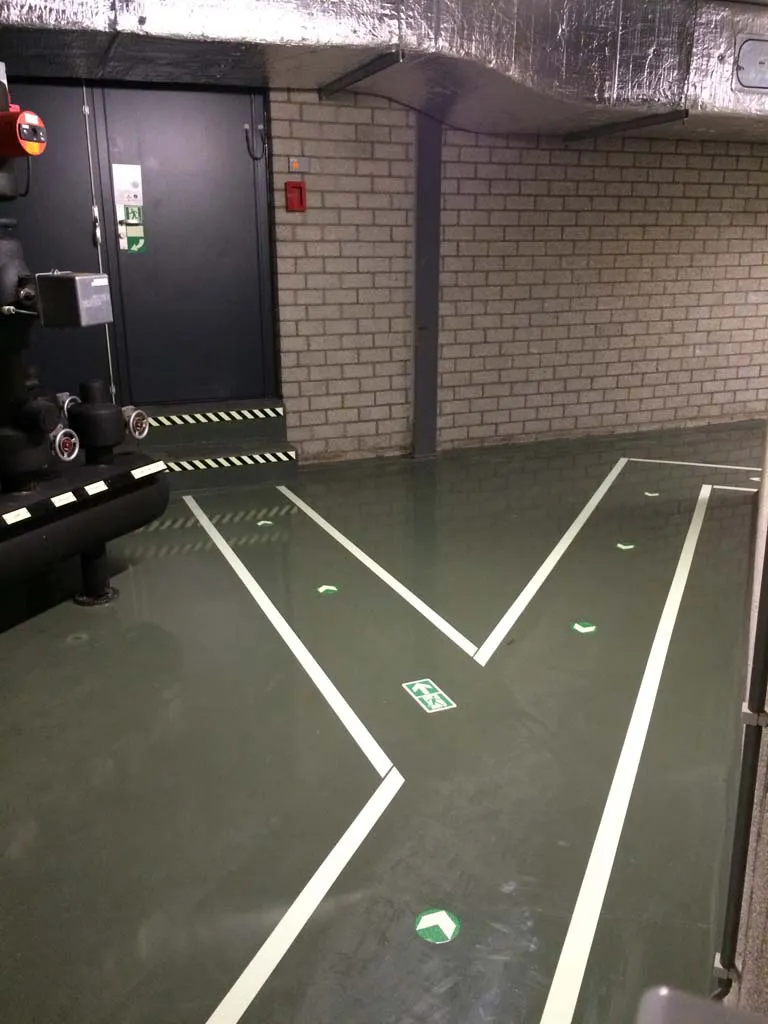
Photoluminescent floor markings can provide supplementary low-level guidance along emergency routes. Possible applications include:
- Exit paths
- Corridor edges
- Stair access
- Emergency doors
- Direction arrows
These markings should complement required emergency lighting, exit signs, and fire safety systems rather than replace them.
Machine Safety Zones
Factories often need clear boundaries around equipment. Photoluminescent markings can be used to define:
- Machine clearance zones
- Maintenance areas
- Restricted access areas
- Inspection zones
This can help reinforce visual separation between machinery and pedestrian movement.
Loading and Logistics Areas
Loading areas often combine:
- Trucks
- Forklifts
- Pallets
- Workers
- Storage equipment
Photoluminescent lines may be used around:
- Loading dock edges
- Walking routes
- Restricted zones
- Equipment boundaries
These areas usually require strong wear resistance and skid resistance.
Storage Aisles
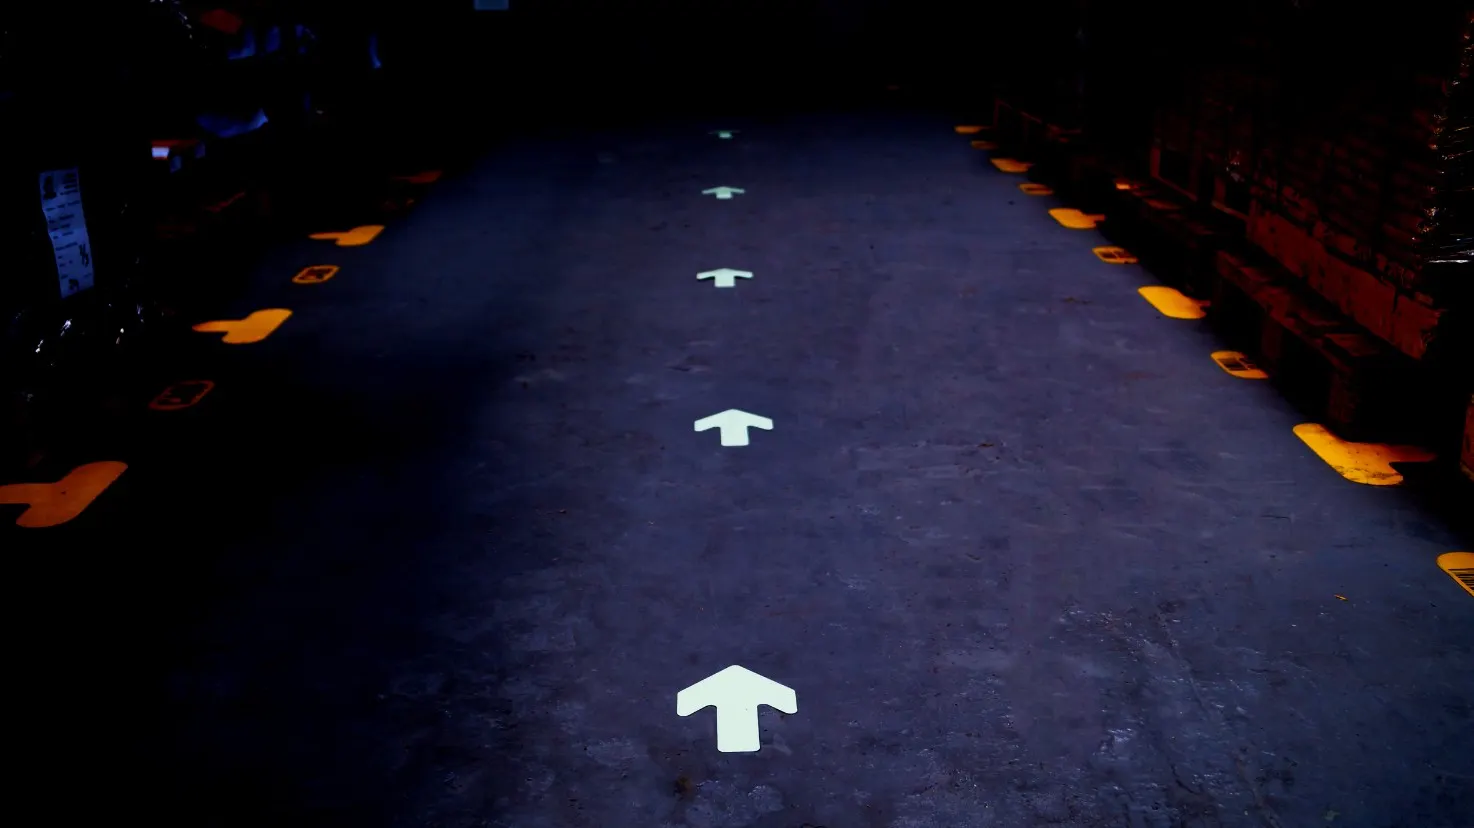
Long warehouse aisles can benefit from continuous low-level guidance. Photoluminescent markings may help define:
- Aisle edges
- Walking routes
- Exit direction
- Storage boundaries
In large warehouses, lighting conditions can vary from one aisle to another, so site testing is important.
Stairways and Level Changes
Stairs, ramps, and raised platforms are important areas to mark. Photoluminescent materials can be used on:
- Stair nosings
- Step edges
- Ramp boundaries
- Platform edges
The marking should remain flat, durable, and slip resistant.
Check charging under the actual facility lights
Unlike outdoor road markings, industrial floor markings often rely primarily on artificial lighting. Performance depends on:
- Lamp type
- Light intensity
- Distance from the floor
- Exposure duration
- Position of the marking
A line directly under a ceiling light may charge more effectively than one under shelves or behind equipment.
Not Every Area Charges Equally
A common mistake is assuming the entire facility will produce the same glow. Charging may be weaker in:
- Dark corners
- Under storage racks
- Behind machines
- Areas far from lights
- Covered loading areas
For large industrial projects, test several representative locations.
Assess the floor and substrate compatibility
Photoluminescent industrial markings may be applied to different substrates depending on the system. Common surfaces include:
- Concrete
- Epoxy floors
- Resin floors
- Cement-based surfaces
- Existing coated floors
The primer and binder should be compatible with the substrate.
Concrete Floors
Concrete is one of the most common industrial substrates. Before application, check for:
- Dust
- Moisture
- Oil
- Weak surface layers
- Cracks
- Old coating residue
Mechanical cleaning or grinding may be necessary.
Epoxy Floors
Existing epoxy floors may provide a smooth and stable surface, but compatibility still needs to be tested. The surface may require:
- Cleaning
- Light abrasion
- Compatible primer
Applying directly over a glossy contaminated floor can reduce adhesion.
Select the base coat, binder and pigment ratio
Photoluminescent coatings often perform better over a white or light-colored base. A typical system may include:
Industrial Floor
↓
Primer
↓
White Base Coat
↓
Photoluminescent Layer
↓
Transparent Protective Topcoat
The light-colored base can improve the apparent glow.
Binder Selection
The luminous pigment needs a compatible binder. A suitable binder should provide:
- Good transparency
- Strong adhesion
- Wear resistance
- Chemical resistance
- Water resistance
- Suitable curing
Industrial floors can be demanding, so durability is especially important.
Pigment Concentration
Too little photoluminescent pigment can produce weak glow. Too much pigment can affect:
- Flow
- Adhesion
- Surface strength
- Application quality
The correct ratio should be tested as part of the complete coating system.
Balance traction, chemical resistance and traffic wear
Industrial floors should not become slippery. This is especially important in:
- Loading areas
- Ramps
- Wet zones
- Pedestrian routes
- Workshops
Anti-slip aggregate may be added to the coating system where needed. The ideal system balances:
Glow Performance + Traction + Durability
Chemical Resistance
Industrial floors may be exposed to:
- Oil
- Cleaning chemicals
- Grease
- Production residue
The coating system should be selected according to the expected chemical environment. A material suitable for a warehouse may not automatically be suitable for a chemical workshop.
Wear Resistance
Industrial traffic can be much more demanding than pedestrian use. Common sources of wear include:
- Forklifts
- Pallet trucks
- Carts
- Machinery
- Repeated foot traffic
High-wear zones require stronger coating systems.
Avoid Main Wheel Paths Where Possible
Repeated forklift turning can create strong abrasion. Where practical, photoluminescent lines can be positioned beside the main wheel path instead of directly under continuous tire movement. This can help extend service life.
Prepare, install and cure the complete system
Good surface preparation is essential. Before application, the floor should normally be:
- Clean
- Dry
- Stable
- Free from oil
- Free from dust
- Free from loose coating
Poor preparation is one of the most common causes of peeling and early failure.
Typical Installation Process
A basic installation may include:
Step 1: Inspect the Floor
Check for moisture, cracks, oil, dust, and existing coating damage.
Step 2: Clean and Prepare
Remove contamination and create a stable surface.
Step 3: Apply Primer
Use a primer compatible with the floor.
Step 4: Apply White Base Coat
Create a light-colored background for stronger glow.
Step 5: Apply Photoluminescent Layer
Apply the luminous coating evenly.
Step 6: Add Anti-Slip Aggregate
Use compatible aggregate where required.
Step 7: Apply Protective Topcoat
A transparent topcoat can improve durability and cleaning resistance.
Curing Before Traffic
The coating should be allowed to cure fully before reopening the area. Premature traffic can damage fresh markings. This is particularly important in facilities with:
- Forklifts
- Carts
- Heavy equipment
The installation schedule should consider operational downtime.
Clean, inspect and repair the markings
Industrial floors collect contamination quickly. Common examples include:
- Dust
- Tire marks
- Oil
- Grease
- Production residue
These contaminants can block light and reduce charging performance. Routine cleaning helps keep the luminous surface exposed.
Maintenance Inspection
Check the marking periodically for:
- Wear
- Peeling
- Cracking
- Reduced glow
- Surface contamination
- Topcoat damage
Local repair is usually easier than waiting for large sections to fail.
Compare photoluminescent, reflective and LED guidance
Photoluminescent vs. Reflective Floor Marking
Reflective and photoluminescent markings work differently.
Reflective Marking
Requires external light to become highly visible.
Photoluminescent Marking
Stores light beforehand and releases afterglow later. In some industrial environments, the two technologies can complement each other.
Photoluminescent vs. LED Guidance
LED systems actively produce light. Photoluminescent markings provide passive afterglow.
Photoluminescent Marking
- No wiring required for afterglow
- Integrated into the floor
- Passive operation
- Lower system complexity
LED Guidance
- Requires power
- Produces stronger active illumination
- More complex installation
- Can maintain controlled brightness
The right choice depends on the facility.
Keep required emergency lighting and safety markings
Can Photoluminescent Markings Replace Emergency Lighting?
No. They can provide supplementary floor-level guidance, but they do not illuminate the entire space. They cannot replace required:
- Emergency lighting
- Exit signage
- Fire safety systems
- Building safety requirements
They should be treated as an additional visual guidance layer.
Can They Replace Standard Industrial Floor Markings?
Not automatically. Factories and warehouses may have specific requirements for:
- Safety colors
- Line width
- Hazard zones
- Pedestrian routes
- Emergency access
Photoluminescent materials should be integrated into the existing safety system rather than replacing required markings without review.
Test the complete system before full installation
Before applying the material across an entire facility, create a small test area. Use the actual:
- Floor
- Primer
- Base coat
- Luminous coating
- Anti-slip system
- Topcoat
Then evaluate:
- Daytime appearance
- Charging under existing lights
- Nighttime glow
- Adhesion
- Skid resistance
- Forklift wear
- Cleaning resistance
Industrial applications at a glance
Photoluminescent industrial floor markings can be particularly useful for:
Warehouses
Pedestrian lanes and emergency routes.
Factories
Machine boundaries and internal walkways.
Logistics Centers
Loading zones and directional guidance.
Workshops
Safety zones and equipment boundaries.
Parking Facilities
Pedestrian routes and exit guidance.
Utility Areas
Low-level route identification.
Choose materials for actual floor conditions
Photoluminescent marking for industrial floors can provide useful passive nighttime guidance in factories, warehouses, and logistics facilities. It can be used for:
- Pedestrian walkways
- Emergency routes
- Machine boundaries
- Loading zones
- Stair edges
- Storage aisles
The best results depend on the complete system:
Correct Surface Preparation + Suitable Primer + White Base + Photoluminescent Layer + Skid Resistance + Durable Topcoat + Proper Lighting
For industrial projects, the most important step is to test the material under the actual lighting, traffic, and cleaning conditions before full installation.
FUXIN supplies Photoluminescent Pigments, Industrial Floor Marking Materials, Glow Safety Coatings, and Luminous Pavement Systems for factories, warehouses, parking facilities, pedestrian routes, and low-light industrial applications.
For samples, quotations, or project material recommendations, please contact us.